English
 Spanish
 Portuguese



JPSK CNC-200-9P CNC Busbar Punching Shearing LineAutomatic feeding, automatic po
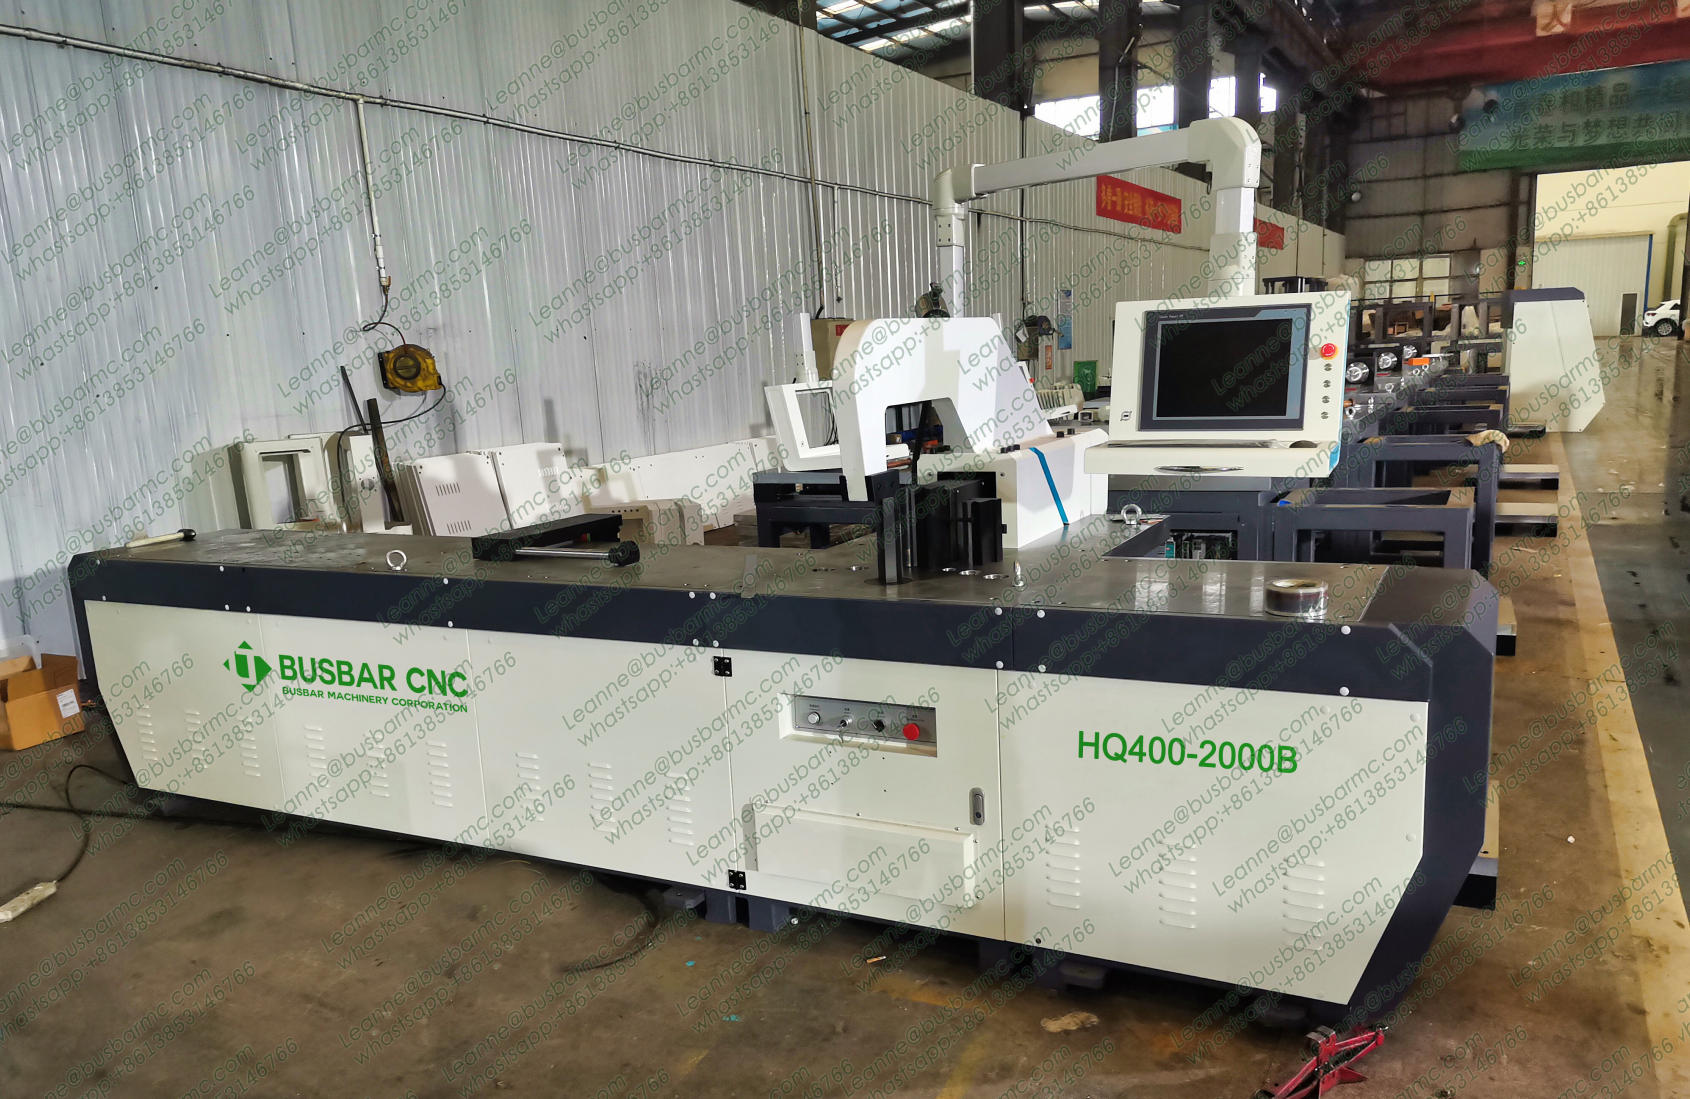
The HQ600-7P is the CNC punching and shearing line to choose when the production bottleneck is gauge changeover on long bars rather than punching speed: one clamp holds the bar for every hole. The series covers two ranges — the 400 kN model processes bars up to 12 × 160 mm, and the 600 kN model reaches 15 × 200 mm, with hole diameters of Φ4.3–25 mm and Φ4.3–35 mm respectively. Each head carries 8 punches and 1 in-line shear blade, with an optional 7-punch plus 1-emboss set. Positioning is servo-controlled on 6 axes with a 2,000 mm X-axis stroke. Stated punching accuracy is ±0.2 mm and positioning accuracy 0.10 mm per 500 mm. Typical application: switchgear, distribution panel and substation busbars.
Values per the model datasheet. Each paragraph is self-contained and states the test condition, the value and the comparison baseline.
Test condition: bar clamped once, processed on the 600 kN model with a 15 × 200 mm bar and on the 400 kN model with a 12 × 160 mm bar. Value: 120 to 150 holes per minute on the 600 kN model and 100 holes per minute on the 400 kN model. Comparison baseline: a single-die punching machine, whose rate is capped by die changes and by manual repositioning of the bar after every hole. Effect: holes per minute stop depending on the operator.
Test condition: bars up to 2,000 mm long clamped once under 6-axis servo control. Value: ±0.2 mm punching accuracy and 0.10 mm positioning accuracy per 500 mm. Comparison baseline: manual template punching, where deviation accumulates with every repositioning of the part. Effect: identical parts in serial production, with no reaming rework.
Test condition: no-load travel over the 2,000 mm X axis, the 860 mm (400 kN) or 960 mm (600 kN) Y axis and the 200 mm or 310 mm Z axis. Value: 75 m/min on the X axis of the 600 kN model and 60 m/min on the 400 kN model, with Y and Z at 35 m/min. Comparison baseline: previous-generation motorised positioning tables, typically restricted to slow long-stroke travel. Effect: dead time between holes drops, so the cycle becomes punch-dominated instead of travel-dominated.
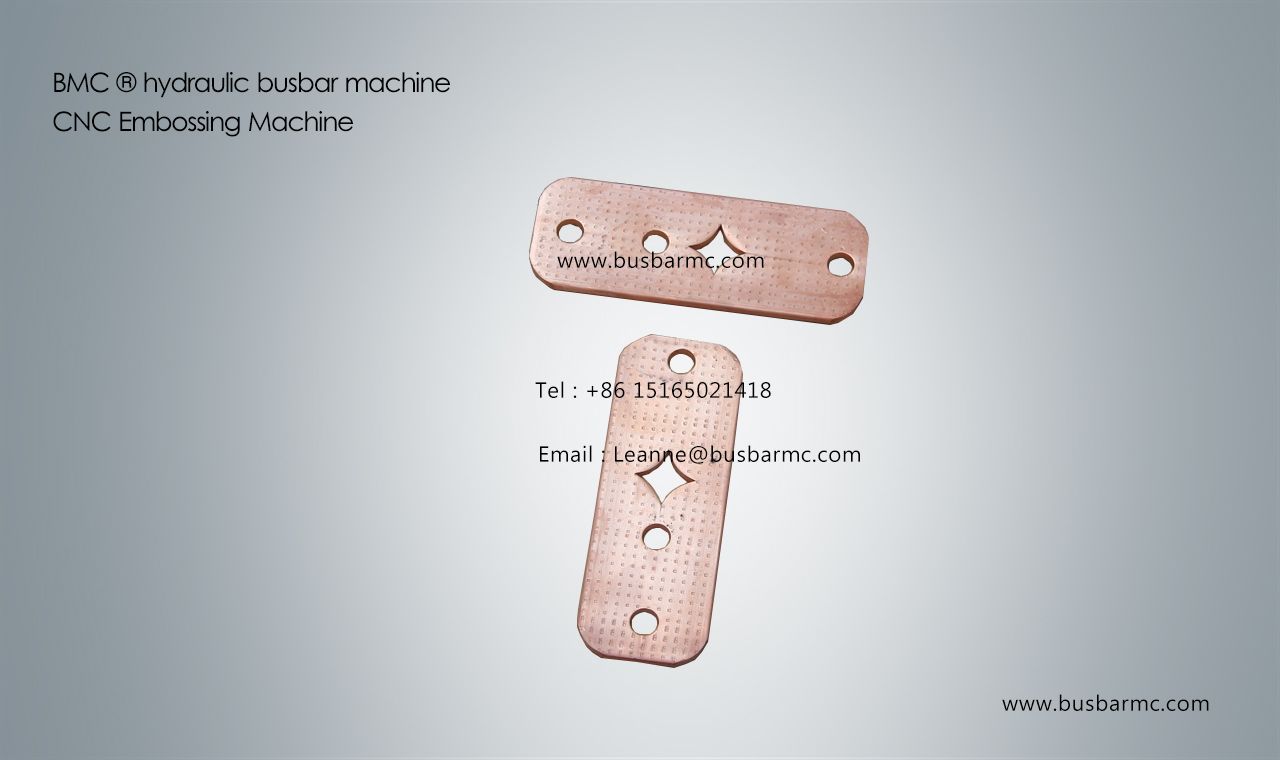
Test condition: one bar with holes of several diameters in a single cycle. Value: 8 punch sets plus 1 shear blade mounted in line, plus 1 maintenance tool set, with a 7-punch plus 1-emboss option. Comparison baseline: a single-die head, which needs one manual change per hole diameter. Effect: a bar with holes of four different diameters is completed without a tooling stop.
The 400 kN model processes bars up to 12 × 160 mm with holes of Φ4.3–25 mm at 100 holes/min. The 600 kN model reaches 15 × 200 mm with holes of Φ4.3–35 mm, at 120 to 150 holes/min and 75 m/min on the X axis.
No. The servo system locates the punching coordinates automatically on 6 axes, with ±0.2 mm punching accuracy, which removes manual marking and templates.
Six CNC axes, with a 2,000 mm X-axis stroke, an 860 mm or 960 mm Y-axis stroke and a 200 mm or 310 mm Z-axis stroke, depending on the power class.
HQ600-SP CNC Busbar Punching Shearing Line
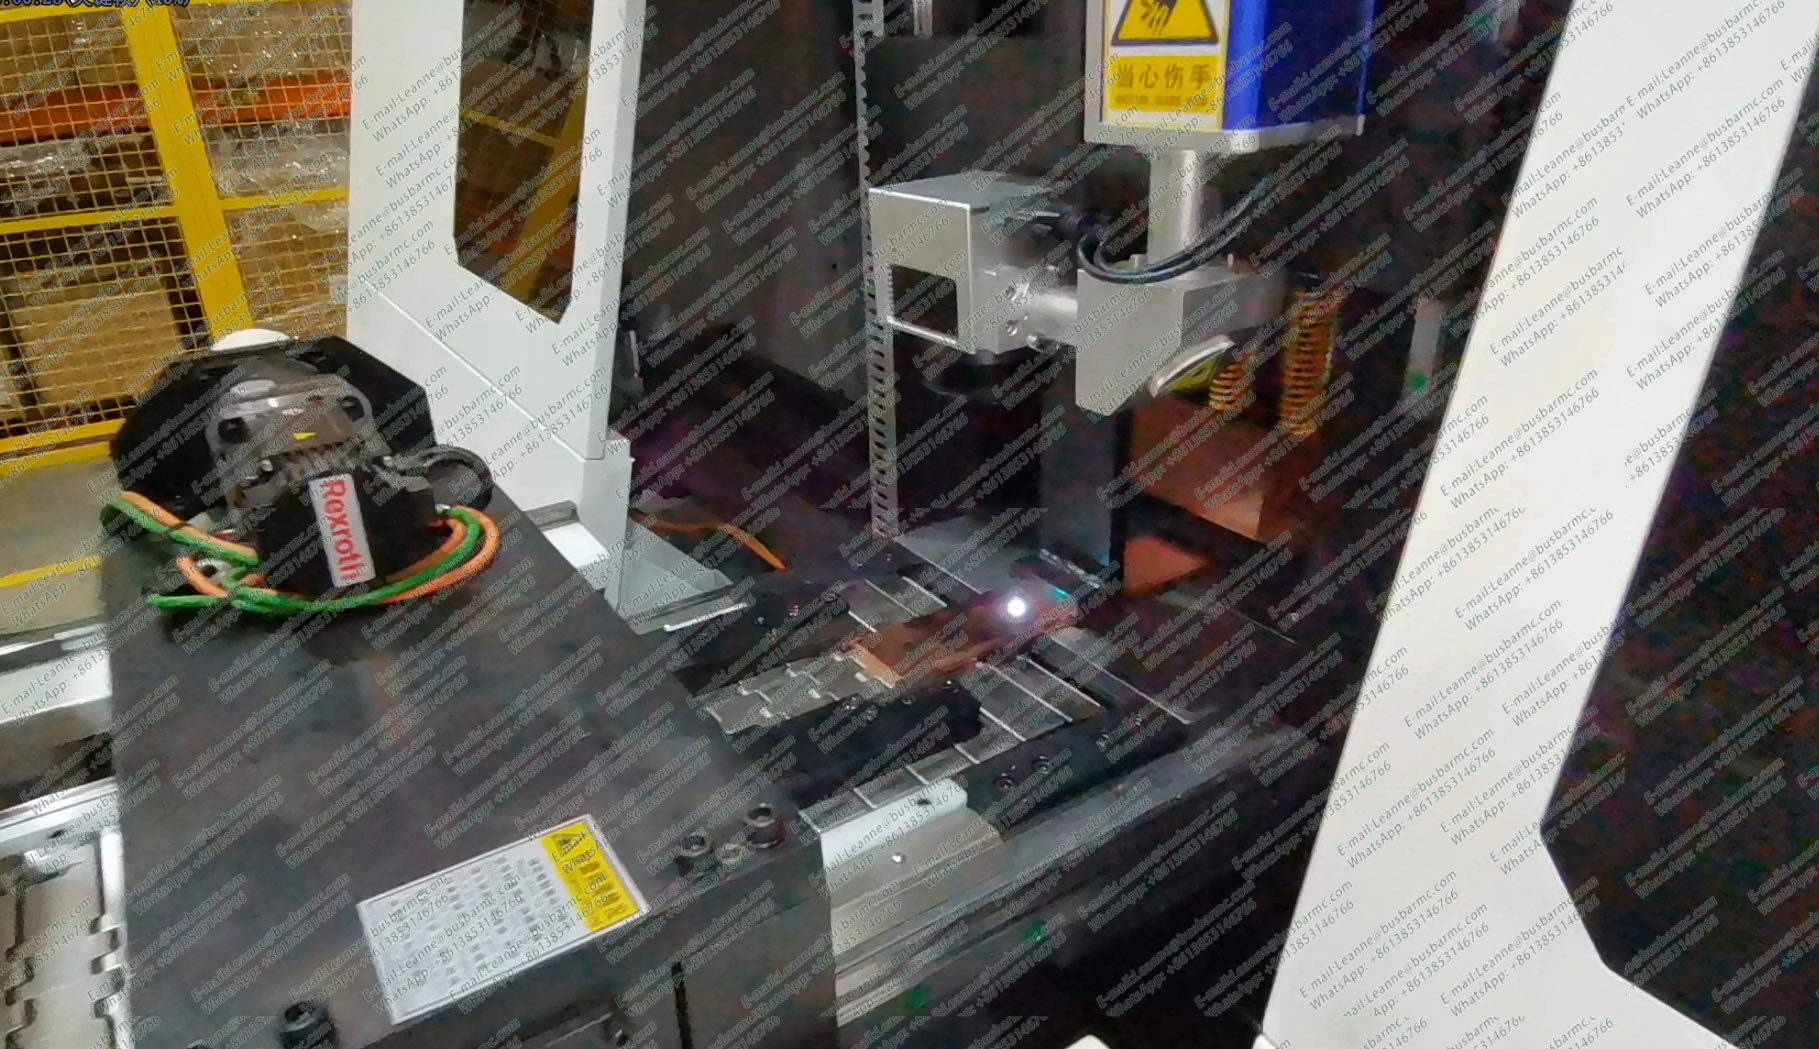
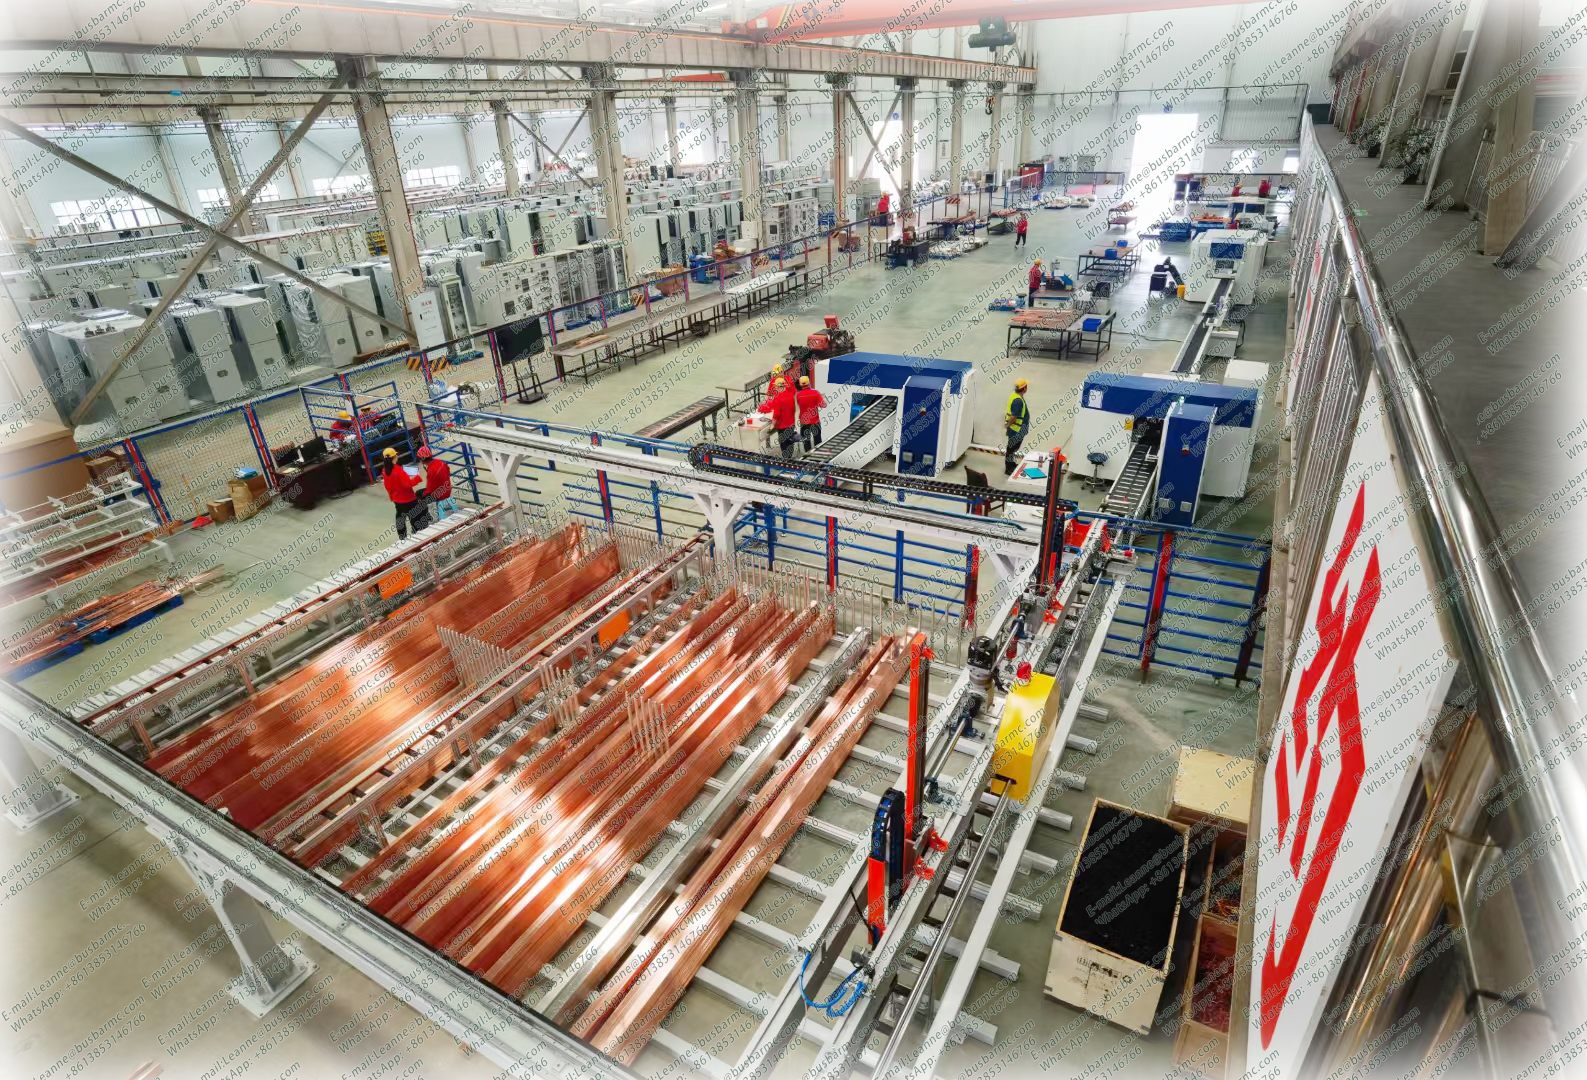
Automatic feeding, automatic positioning, automatic clamping, automatic punching, automatic shearing, automatic replacement of mold, automatic delivery CNC busbar punching cutting line.
More details please kindly contact us freely
LT CNC Machinery
E-mail: [email protected]
Whatsapp: +8613853146766
Wechat: +8613853146766
www.busbarmc.com
Products:
CNC 3in1 Busbar Processing Machine
CNC Servo Busbar Bending Machine
CNC Busbar Punching and Shearing Machine
Portable Busbar Machine
Widely used in high and low voltage switchgear, switchboard, transformer manufacturing,box-type substation, busway and other electric power industry.
Hot Tags: HQ600-SP cnc busbar punching shearing line, China, suppliers, manufacturers, factory, price